We recommend identifying the installed wrapper and seal arrangement before using a forming-collar checklist. Horizontal wrappers may use a forming box or other former; vertical machines use a different product path. Even the intended fin or lap seal changes which film surfaces meet.
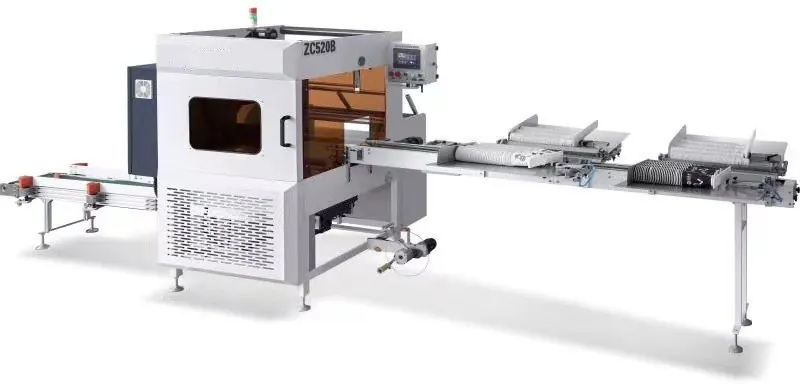
Separate machine completeness from a seal recipe
In the used flow-wrapper discussion, film-handling and sealing complaints occurred alongside a reported product-support problem. The poster later reported missing parts. We would check the delivered parts and threading diagram before copying a sealing-temperature suggestion. The account does not establish one cause for every symptom.
Setup must use the approved film and pack format. This guide does not publish universal collar gaps, temperatures or overlap values. Keep heaters and motion isolated during mechanical adjustment and follow the installed machine procedure.
Decision matrix
| Setup input | Evidence | Decision |
|---|---|---|
| Film | Width, thickness, seal layer, artwork and roll condition | Matches the approved bag format |
| Former | Part ID, centerline, cleanliness and mounting datum | Creates the intended tube geometry |
| Web entry | Roll center, idlers, tension and edge position | Presents film symmetrically |
| Pull/seal | Belt/roller contact, overlap and sealer center | Carries and seals without lateral force |
| Trial pack | Seam position, wrinkles, seal integrity and cut relation | Approves the complete format |
Verify film and former identity
Match film code, width, thickness, sealable surfaces, print repeat and winding direction to the actual fin- or lap-seal job. Confirm the actual former and any tube or related change parts supplied for this architecture by their controlled part references. Similar bag widths may still require different geometry for product diameter or film behavior.
Inspect the former surfaces and edges for adhesive, scratches, dents and tape residue. Clean only with the approved method. A rough contact point can drag one side of the film and imitate poor centering.
Establish the machine centerline
Use the defined former or product-tube datum, not a visually convenient frame edge. Verify the installed former and transport references against the machine-specific datum and sealing path. Record mounting scales or measured references before adjustment so the known setup can be recovered.
Use the installed wrapper’s forming and longitudinal-sealing references together. A vertical-wrapper example does not establish a horizontal cup-packer setup. Do not shift the center sealer to chase a changing overlap until entry and former alignment are stable.
Present film without lateral steering force
Check the unwind and the guides or tension devices actually fitted against the supplied threading diagram; not every wrapper uses a dancer. Observe edge position before the collar. If the web moves laterally upstream, use the linked tracking guide to correct roll, roller or tension causes.
Adjust entry guides so they guide without pinching. Film should wrap the former smoothly with balanced contact and no isolated hard crease. Use permitted non-contact references to identify where a wrinkle begins; any off-machine sample marks must be approved for the film and packaging application.
Align pull belts and center seal
Where fitted, inspect the supplied film-driving belts or rollers and their documented contact references; do not import a vertical-machine pull-belt method. Unequal pressure or wear can rotate the tube after the collar. Set the intended film overlap from the approved pack drawing, then align the longitudinal sealing unit to that stable overlap.
Keep temperature and pressure at the validated recipe while making geometry trials. Changing heat, speed and collar position together makes the cause impossible to identify. Inspect for trapped folds, channel leaks and print scuffing.
Validate complete packs over a run
Follow the supplier-approved trial sequence and verify the intended released operating condition. Measure seam location around the pack, overlap, bag width, end-seal relationship and cut position. Inspect startup, stop/restart and steady-running samples.
Record film lot, former ID, datums, tracking and accepted samples. Send HANNAI the film specification, pack drawing and marked defect sequence when support is needed. A correct forming setup must remain stable, not merely produce one acceptable bag.
Follow the overlap from the last stable point
Confirm the approved film code, winding direction, sealable surfaces, format drawing and former/change-part identity. Observe the web edge at permitted references before and after forming. If overlap begins changing before the sealing unit, moving that unit may follow the symptom without stabilizing the film.
Retain startup and steady-running samples with the seam side and travel direction identified. For an approved comparison, record the original datum and change one permitted geometry setting at a time. Omron’s horizontal flow-wrapper overview is the appropriate architecture reference here, replacing a vertical-wrapper example. It does not identify which belts, rollers, dancers or former are installed on your machine.
Discuss the evidence with HANNAI
Send the actual wrapper model, film specification, seal type, threading diagram, former identification and marked pack sequence through our inquiry page. Confirm geometry before requesting a new heat or pressure recipe.