Paper bowl machine bottom wrinkles need a location map before a pressure change. A fold near the side seam may have a different cause from uneven gathering around the whole base. The useful question is where the unwanted fold first appears and how it relates to the disc, sidewall skirt and forming-tool position.
This guide concerns unintended bottom folds on a construction whose approved sample and drawing define the required base profile. It does not classify every formed texture as a defect. Normal tooling impressions, coating damage and an open leak path must be recorded separately.
Diagnostic decision table
| Wrinkle pattern | First comparison | Diagnostic boundary |
|---|---|---|
| Repeated at side seam | Material stack and seam orientation | Local thickness or presentation |
| Repeated at one machine direction | Tool and transfer reference | Station-specific contact |
| Uneven folds around the base | Disc centering and skirt geometry | Material presentation before forming |
| Appearance changes with material lot | Approved blank and disc samples | Input variation versus setup |
Define the unacceptable feature with a reference sample
Compare the suspect bowl with the approved base profile under consistent lighting. Mark the side seam and assign a simple clock orientation to each sample. Record whether the feature is a raised fold, a depressed tool mark, a tear or a displaced disc.
Use the customer quality plan to decide which appearance and integrity conditions require containment. A photograph alone cannot establish whether a fold forms a liquid path. Retain untested samples for geometry inspection and separately identified samples for the agreed destructive or leak tests.
Locate the earliest affected process stage
Use guarded observation and the supplier-approved stopped-machine sampling procedure to compare presentation before bottom forming with the discharged bowl. Do not reach into a station to retrieve a partly formed sample. Where safe intermediate sampling is unavailable, ask the supplier for a diagnostic method.
Keep station identity, tooling position and material lot attached to every sample. If a fold is already present before the final knurling operation, increasing knurling pressure is unlikely to explain the upstream origin. If it appears only after a particular stage, concentrate inspection on that stage and its incoming geometry.
Compare disc and sidewall geometry as a matched set
Check bottom disc diameter, edge condition, centering and orientation against the approved drawing and process. Compare the sidewall skirt length and its consistency around the bowl. These dimensions must be assessed as a matched construction rather than optimized independently.
Look for distorted or doubled discs, damaged edges and side-seam thickness changes. Measure representative incoming material with the agreed method and preserve accepted samples from the preceding lot where available. Do not trim discs or shorten skirts by an arbitrary amount to make a single sample look smoother.
Map tooling contact without changing every setting
After energy isolation and safe cooling, inspect the relevant forming surfaces for buildup, wear and local damage. Compare the position of each repeated fold with tool orientation. Review centering and transfer support before altering the heating or pressure recipe.
Treat thermal condition, contact geometry and material presentation as separate trial factors. Maintain a record of the original approved settings, and change only a verified factor within the supplier procedure. A visually smoother base obtained by excessive force may conceal coating damage or an incorrect bottom profile rather than improve the finished bowl.
Verify base appearance and integrity independently
Repeat representative startup and steady-running samples after correction. Map the same locations and compare the base geometry using the original reference method. Conduct the specified leak and handling tests under their defined fill, conditioning and observation conditions; do not invent a universal test duration.
Confirm that the correction has not introduced disc movement, base rocking, rim distortion or poor nesting. Send HANNAI the bowl drawing, disc measurements, orientation-marked photos and stage-by-stage evidence. The result should identify whether the next correction belongs to material preparation, transfer alignment or bottom-forming tooling.
Related equipment and next checks
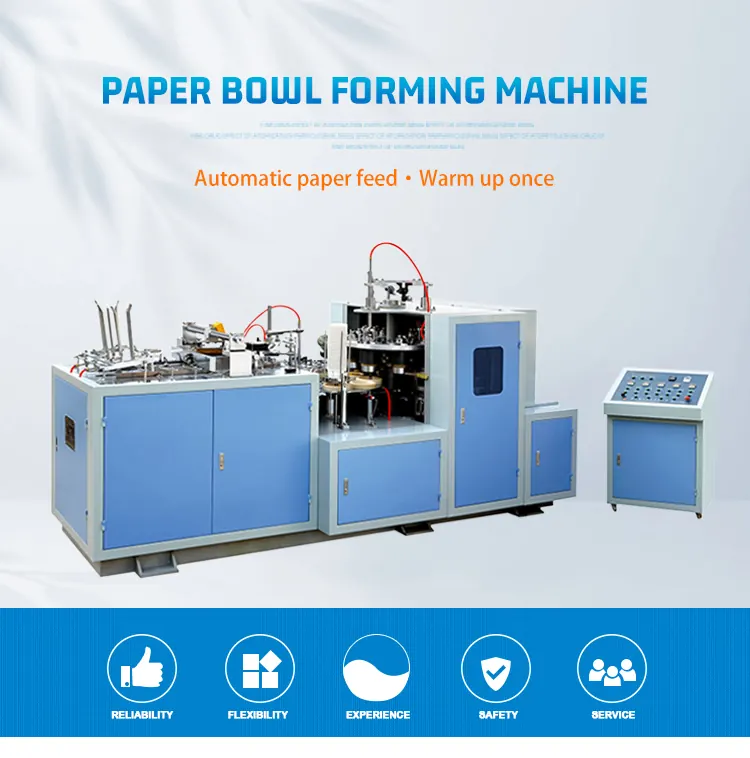
Review the paper bowl forming machine and the related guide to bottom disc feeding and sealing. The Engineering Notes archive connects these checks with wider machine planning.
Frequently asked questions
Are all bottom marks wrinkles?
No. Separate intended tooling texture from unwanted folds and damage.
Should knurling pressure be increased first?
First locate the stage where the fold appears.
Can a smooth-looking base still leak?
Yes. Appearance and integrity require separate checks.
Why mark the side seam on each sample?
It allows local material thickness and machine-direction patterns to be distinguished.
Review the evidence with HANNAI
Send your machine model, component identification and the observations described in this guide. Include the drawing or material reference and any before-and-after measurements so the required next check can be identified.