The linear guide rail, slider carriage, mounting surface and driven member is a small part of a larger manufacturing sequence, but it can influence rough travel, side play, repeat-position variation, abnormal noise or uneven tooling contact. A reliable diagnosis should begin with repeatable system observations rather than a replacement guess. This guide gives maintenance teams a structured way to isolate the status while preserving the delivered system references.
A practical paper cup machine linear guide rail wear review should connect the visible symptom with the command, physical response and finished output. Final limits, parts and adjustments remain configuration-specific; use the provided assembly drawing, guide manufacturer instructions and system alignment process instead of applying a universal value.
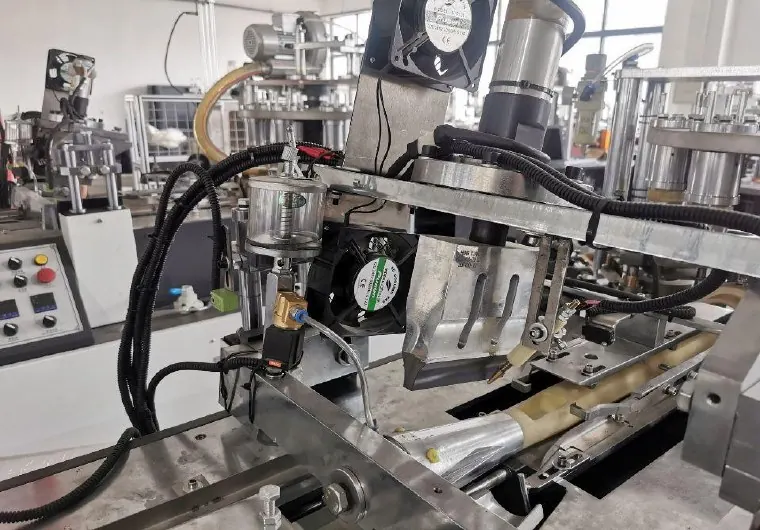
Separate the symptom from its consequences
Note rail and carriage model, axis location, lubrication point, mounting arrangement and the tooling carried by the axis. Mark when the concern appears during unloaded manual movement where permitted, slow cycle, warm manufacturing and direction reversal. Include the operator observation, system state, paper input or job identity and the last known acceptable manufacturing period. This prevents several different faults from being grouped under one general alarm or quality description.
Keep samples or videos in sequence and label the system position, direction and time. A pattern tied to one station, one direction, one speed transition or one paper input lot is more useful than a mixed collection of rejected output. Review the relevant context in the bearing status monitoring guide before changing a setting.
Inspect wear patterns before cleaning them away
| Observed status | Observations to collect | Diagnostic direction |
|---|---|---|
| Roughness occurs at one travel position | Cleaned rail map, carriage location and repeatable motion video | Local dent, contamination or rail damage |
| Play changes with direction | Referenced indicator readings and load direction | Carriage clearance, fastener or support movement |
| One rail edge shows a polished band | Wear pattern, mounting face and adjacent tooling load | Misalignment or side loading |
| Lubricant becomes dark quickly | Lubrication note, wiper status and contamination source | Ingress, wear debris or unsuitable lubricant |
| Tool contact varies after service | Rail reference, shim note and station dimensions | Mounting or parallelism change |
Control hazardous energy and preserve references
Apply the site lockout and isolation process for electrical, pneumatic, vacuum, thermal, gravity and stored mechanical energy that applies to this equipment. Verify the zero-energy state before guards, terminals, tubing, tooling or drive components are accessed. Hot surfaces and charged electrical parts may remain hazardous after the system stops.
Photograph connectors, tube routing, witness marks, adjustment positions, wiring labels and part orientation before disassembly. Qualified personnel should perform live electrical or pressure dimensions only when the accepted diagnostic process specifically requires them and appropriate controls are in place.
Inspect the part in its complete load path
Inspect wipers, grease ports, rail fasteners, mounting shoulders, coupling members and cable or hose drag. A carriage can feel loose because the support plate moves, while a tight axis may be distorted by parallel rails or an uneven mounting face.
Clean only by the established method and preserve deposits, wear bands, damaged parts or filter debris when they may explain the event. Replacement parts must match the provided identification and service requirements. A visually similar part can have different electrical, pneumatic, thermal, dimensional or paper input characteristics.
Compare command, response and finished output
Place the command observations beside the physical response: controller output, valve or drive state, sensor transition, pressure or temperature behavior, motion and final formed piece. The sequence shows whether the part failed to receive a command, received it but did not respond, or responded correctly while another process variable created the defect.
Use calibrated or verified instruments appropriate to the provided process. Note measurement location, instrument resolution, system state and repeated results. Avoid converting a single observation into a tolerance; acceptance criteria must come from accepted drawings, manuals, paper input data or an agreed known-good baseline.
Rule out interacting system and paper input causes
Examine upstream preparation and downstream handling before closing the diagnosis. Paper input identity, contamination, alignment, lubrication, air or electrical supply, timing, load and recent maintenance can change how the part behaves. The coupling and shaft alignment guide provides a related system examine that can prevent a local repair from masking the original source.
Change one controlled variable at a time and log the before-and-after response. If several adjustments are made together, a short improvement cannot be attributed to one cause, and the fault may return when speed, temperature, roll diameter or manufacturing demand changes.
Choose corrective work from established observations
Classify the finding as contamination, connection, wear, misalignment, supply, control, paper input or configuration. Then match the corrective action to the part documentation and the system supplier’s guidance. Do not bypass an interlock, increase a setpoint beyond its accepted range or modify a safety-related circuit to keep manufacturing running.
Where the observations is incomplete, preserve the system state and send a compact observations pack for review. It should contain system and part identity, annotated photos, a sequence video, readings with locations, alarms, paper input or job data, recent service history and representative good and bad output.
Verify the repair in stages
Before power or pressure is restored, validate tools are removed, connections are secure, guards are reinstated and the work area is clear. Use the established manual, jog or slow-cycle examine first, then progress through small controlled manufacturing stages while watching the original symptom and any secondary effect.
Validate smooth travel through the full permitted stroke, repeat position from both directions, monitor noise and temperature, then evaluate station-marked cups during a controlled run. Do not release the system based only on one acceptable cycle. Document the parts or adjustments changed, final observations, retained samples and the person authorized to return the equipment to manufacturing.
Prevent recurrence with a traceable maintenance note
Add the confirmed inspection point to the maintenance plan with an objective method and a reference source. Trend the status by time, cycles or manufacturing demand as appropriate, but do not invent a replacement interval. Part status, environment, paper input and system loading should determine the review frequency.
Link the maintenance note to alarms, manufacturing samples and spare-part identity. This makes future troubleshooting faster and helps purchasing teams order the correct configuration instead of a visually similar substitute.
Frequently asked questions
Should a rail be polished when a rough spot is found?
No. Preserve the observations and follow the part process; uncontrolled abrasion can damage the raceway geometry.
Can grease be added until the noise disappears?
No. Validate the specified lubricant, quantity, interval and contamination status. Overfilling can create other problems.
Is carriage replacement enough when wear is visible?
Not always. Rail status, mounting accuracy, loading and lubrication cause must be reviewed as a system.
How should play be compared?
Use the established reference, load direction and instrument method, then compare with provided data or a verified known-good axis.
Send the system model, part identity, labeled samples, sequence video, dimensions and service history through our inquiry page. HANNAI can review the observations against the provided system configuration.