Paper cup packing film friction can influence whether a bag slides through the forming path, grips the drive surfaces or stacks consistently. Two films with similar thickness and seal behavior may run differently. Identify the contacting surfaces before deciding that a higher or lower coefficient of friction is automatically better.
This guide connects a supplier or laboratory friction report with a controlled machine trial. It does not specify a universal coefficient, test speed or machine setting. Select the applicable method and acceptance range with the film supplier and packaging equipment supplier.
Diagnostic decision table
| Symptom | Surface pair to investigate | Separate from |
|---|---|---|
| Film hesitates at startup | Film against relevant guide surface | Unwind resistance |
| Film slips at a drive section | Film against the actual traction surface | Incorrect drive condition |
| Bags slide in a stack | Outer film against outer film | Stack geometry and trapped air |
| Bags resist separation | Contacting film faces | Blocking or seal interaction |
Identify the film construction and contacting faces
Record film supplier, grade, lot, thickness designation, manufacturing or conversion date where supplied, and which face is inside the bag. Identify printing, treatment or coating on each surface. A report labelled film COF is incomplete if it does not state what was sliding against what.
Map the relevant machine contacts: forming collar, fixed guides, drive belts and finished-bag surfaces. Film-to-film results may help explain stacking, while film against a specified metal surface addresses a different question. Neither automatically predicts traction against the installed belt material. Keep the surface pair explicit in every comparison.
Review the test report before comparing numbers
Instron describes standardized testing that distinguishes the force needed to initiate movement from resistance during continued sliding. Static and kinetic coefficients represent different aspects of behavior. Record which result is reported and the test method, specimen orientation, conditioning and contacting material used.
Ask the laboratory to confirm that the method applies to the film construction and surface behavior. Sticky or blocking samples may need a different investigation from ordinary sliding friction. Compare reports only when their conditions are compatible; a change in method or surface pair can change the result without any change in the delivered film.
Preserve sample history and handling
Retain samples from suspect and known-good rolls with the same handling procedure. Avoid touching the test surfaces or contaminating them with machine oil, cleaning residue or dust. Keep orientation and location on the roll identifiable. Record storage and conditioning information that the film supplier considers relevant.
If a complaint changes after storage, compare material at defined ages rather than assuming the original certificate describes every later condition. Ask the supplier whether the film formulation requires a defined conditioning interval. Do not apply powder, lubricant or an unapproved spray to make packaging film slide more easily through the machine.
Use a line trial to test the practical effect
Run approved reference and candidate film with the same cup bundle, verified threading and initial machine recipe. Record interruptions, film slip, tracking behavior, bag formation and the defined quality checks. Include both starting and sustained operation if those conditions belong to the intended use.
Keep tension, drive pressure and collar adjustments unchanged for the baseline comparison. If an authorized adjustment is required, document it as a new condition. A film that improves sliding over a guide may reduce traction elsewhere. Evaluate the complete path rather than declaring success at the first station that runs more smoothly.
Approve the film using combined evidence
Combine the applicable friction report with line behavior, sealing quality and handling performance. Define the accepted film construction, face orientation, test method and any approved setup revision. A single COF number does not replace the rest of the packaging-material specification.
Send HANNAI the surface-pair report, film identity, machine-path observations and trial counts if the problem remains unresolved. Include whether the symptom occurs at startup, continuous feed or finished-bag handling. That distinction helps decide whether the next action concerns material friction, unwind mechanics, guide condition or traction without using undocumented machine pressure as a universal cure.
Related equipment and next checks
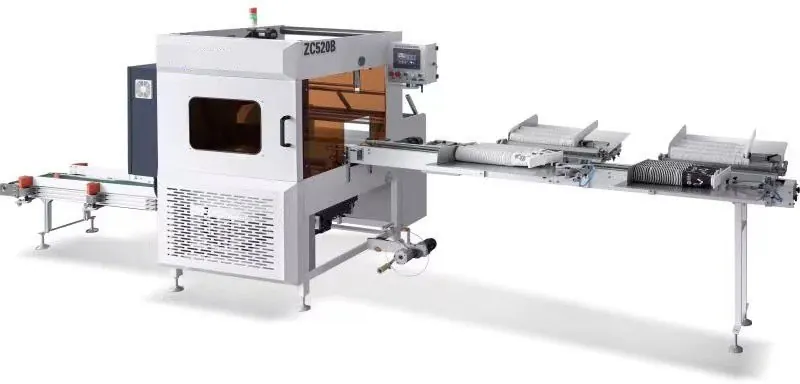
Review the paper cup packing machine and the related guide to film-change and seal validation. The Engineering Notes archive connects these checks with wider machine planning.
Technical reference
- Instron explanation of ISO 8295 plastic-film friction testing — general reference; confirm applicability to the installed equipment.
Frequently asked questions
Is a lower friction coefficient always better?
No. Sliding, traction and stacking can require different behavior.
Does film-to-film COF predict belt traction?
Not directly; the contacting surface pair is different.
Can reports from different test methods be compared unchanged?
Confirm compatible methods, surfaces and conditioning before drawing conclusions.
Does a good friction result approve the complete film?
No. Verify sealing, handling and the other agreed material requirements.
Review the evidence with HANNAI
Send your machine model, component identification and the observations described in this guide. Include the drawing or material reference and any before-and-after measurements so the required next check can be identified.