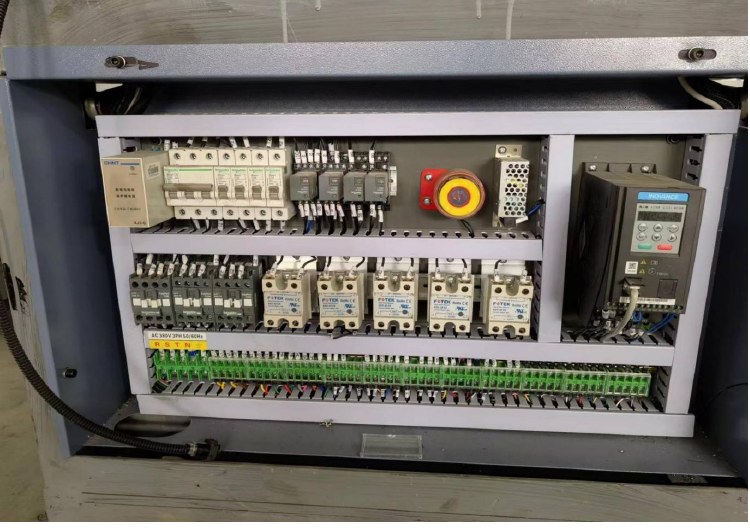
Paper cup machine energy consumption should be measured against a defined equipment and production boundary. Rated power describes an electrical requirement or rating; it does not automatically establish energy used during a shift or cost per accepted cup.
Decide what the measurement should answer before installing or reading a meter. Comparing forming machines, budgeting a complete line and investigating idle operation are different tasks. Record the boundary and retain accepted production from the same interval.
Separate power from energy
Power is a rate, commonly expressed in kW. Energy accumulated over an interval is commonly expressed in kWh. A machine rating multiplied by every scheduled hour is a planning assumption, not measured consumption under the actual operating states.
Obtain the supplier's confirmed electrical requirement for the quoted configuration. Use the voltage requirements guide for site compatibility. Qualified personnel should assess the installation and any temporary or permanent measurement equipment.
Define which equipment the meter covers
Identify whether the reading includes only the forming machine or also collection, packing, upstream equipment and compressed-air generation. Record shared services separately when their contribution cannot be measured directly.
Do not call an allocated compressor cost a direct machine measurement. If an allocation is used for planning, explain the method and uncertainty. Keep the same inclusion rules when comparing configurations or production periods.
| Measurement field | Information to record | Comparison purpose |
|---|---|---|
| Equipment boundary | Metered machine and included auxiliaries | Equivalent scope |
| Time boundary | Start/end readings and operating interval | Matches production counts |
| Operating states | Startup, running, idle and stopped time | Explains consumption differences |
| Application | Cup, material, tooling and configuration | Avoids mixed-product comparisons |
| Output | Accepted and relevant packed counts | Uses the intended denominator |
| Shared services | Metered or allocated basis | Makes assumptions visible |
Read energy and output over the same interval
Retain the initial and final energy reading and the corresponding production record. Define whether startup and idle periods are included. Count accepted cups using the agreed inspection and release boundary rather than a theoretical rate multiplied by shift time.
Energy per thousand accepted cups = included kWh ÷ accepted cups × 1,000. The production-capacity guide helps distinguish running rate from accepted output and packing constraints.
Worked example with declared assumptions
This is hypothetical arithmetic, not a HANNAI consumption figure. An included energy reading of 120 kWh and 30,000 accepted cups gives 4 kWh per thousand accepted cups. At an assumed tariff of 0.15 monetary units per kWh, that included energy cost is 0.60 units per thousand accepted cups.
If the same 120 kWh corresponds to 24,000 accepted cups, the intensity becomes 5 kWh per thousand. That difference alone does not prove the machine is less efficient; longer idle time, a different cup or more rejects may explain it. Retain the operating record before selecting a cause.
Investigate state losses before changing the process
Split consumption by operating states where the measurement method supports it. Look for unnecessary waiting caused by material shortages, delayed inspection or downstream constraints. Identify the reason and responsible process rather than treating all idle time as operator error.
Follow supplier instructions for shutdown, warmup and restart. Turning off a system earlier is not a valid improvement if it compromises cup quality or creates additional startup loss. Do not alter sealing conditions solely to reduce an energy reading.
Compare equivalent applications
Keep cup geometry, material, equipment scope and quality criteria consistent where practical. Record configuration and scheduling differences that cannot be controlled. A lower total kWh can coexist with less accepted output, so retain both figures.
When studying several products, calculate them separately before combining a weighted result. Mixing a small high-volume cup with frequent large-cup changeovers can distort a simple shift comparison. Use enough relevant observations to avoid treating one interrupted run as the normal result.
Translate evidence into a purchasing discussion
Ask the supplier which ratings are available and which operating measurements can be provided for your application. Identify whether a quoted consumption statement includes auxiliaries and what output/quality boundary it uses. Leave missing values open instead of entering zero.
Use the total cost of ownership guide to place measured energy alongside the wider budget. It remains one input in configuration selection, together with accepted output, material suitability and service scope.
Frequently asked questions
Can nameplate power establish shift energy cost?
Not by itself. It supports electrical planning; actual energy depends on operating states and the measurement boundary.
Should compressed-air energy be included?
Include it when the analysis covers that service, and distinguish direct measurement from an allocation.
Why divide by accepted cups?
It connects included energy to production that meets the agreed criteria rather than counting rejected cups as usable output.
Does a smaller kWh reading prove an improvement?
Compare equivalent accepted output and quality conditions. A lower reading with less production may not improve energy intensity.
Request an energy-evidence brief
Send the cup/material specification, shift plan, equipment boundary and available measurements through the HANNAI inquiry page. Ask for configuration-specific ratings and clearly described trial evidence.