Center seal rollers must grip or seal the longitudinal film overlap while the formed tube moves steadily. Uneven contact, worn surfaces, misalignment, contamination or incorrect thermal condition can create channel leaks, wrinkles, tracking force and intermittent pull.
The correct roller gap, pressure and temperature depend on film, coating and machine construction. Use the approved pack specification and installed manual. Isolate motion and hot surfaces before measurement; never place test material into a live nip by hand.
Decision matrix
| Process factor | Evidence | Decision |
|---|---|---|
| Film tube | Width, overlap, entry angle and tracking | Confirm stable geometry before the nip |
| Rollers | Surface, runout, bearings and parallel contact | Identify mechanical cause |
| Force/gap | Adjustment datums and contact pattern | Apply uniform approved pressure |
| Thermal | Set/actual trend and surface distribution | Separate heat from mechanics |
| Samples | Seal position, channels, wrinkles and strength method | Approve repeatable package quality |
Stabilize the film overlap first
Confirm the correct forming collar and film width, then mark the longitudinal overlap before it reaches the rollers. Observe whether overlap changes with roll diameter, speed or stop/restart. A wandering tube cannot be corrected reliably by higher roller pressure.
Use the film tracking and forming-collar guides to resolve upstream centering, tension and pull differences. Record print side and sealing layer so samples are evaluated in the correct orientation.
Inspect roller surfaces and support
With energy isolated and heat controlled, clean the rollers using the approved material. Inspect coating, knurl or smooth surface for wear, cuts, buildup and polished bands. Check shafts, bearings, gears and couplings for play or binding.
Measure runout or diameter only from defined datums. A local high spot can create periodic marking while a bearing or frame issue creates changing contact. Do not grind or sand sealing surfaces at the machine without a repair specification.
Verify parallel contact and pressure
Record adjustment positions and use the machine-approved contact method to compare across roller width. Check that supports and stops move symmetrically. Uneven contact can leave one channel open while the display shows normal pressure.
Adjust in small documented steps and keep film geometry constant. Do not exceed design force to flatten wrinkles created upstream. Confirm guards and nip protection remain functional after every mechanical change.
Separate thermal and speed effects
Compare controller setpoint, displayed process value and safe surface-temperature evidence at stable operating condition. Inspect heater, sensor and wiring if one area remains different. Do not copy a temperature from another film.
Run controlled samples at the approved speed range while holding geometry and pressure constant. Omron packaging research notes that speed, temperature and roller position can jointly affect center sealing; change one factor at a time for diagnosis.
Approve the seal with repeated samples
Inspect seal centering, overlap, wrinkles, contamination, channel leaks and damage. Use the project’s defined seal test rather than a subjective pull. Sample startup, steady production and stop/restart because thermal and tracking conditions change.
Record film lot, roller condition, datums, settings and labeled samples. Send HANNAI the film specification, pack drawing and defect map. The linked jaw guide supports contamination and temperature-uniformity inspection on the transverse seal.
Technical references
- Omron packaging process study — general component guidance; the installed machine documentation remains controlling.
Related machine and guide
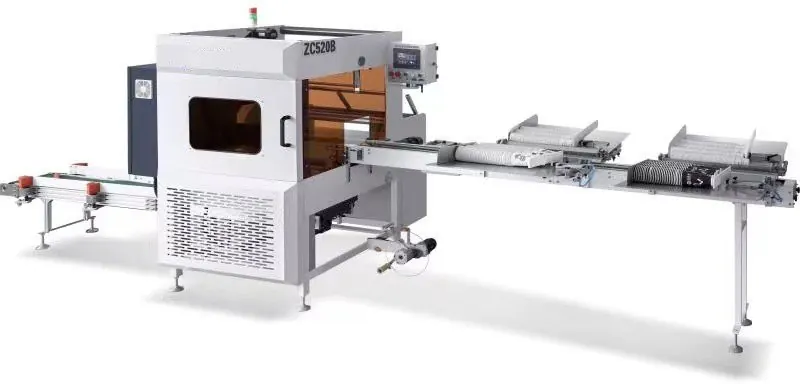
Review the paper cup packing machine for machine context, then use the sealing jaw contamination guide for the adjacent check. Browse all Buyer Guides when building a wider project checklist.
Frequently asked questions
Can higher roller pressure correct changing overlap?
No. Stabilize former, tracking and pull geometry first.
Does displayed temperature prove both roller surfaces are uniform?
No. Verify the actual system with an approved method.
Why sample after stop and restart?
Temperature, tension and film position can differ from steady running.
What indicates parallelism problems?
Uneven contact, one-sided channel leaks, wear bands or cross-web variation.
Review your machine configuration with HANNAI
Send the machine model, project reference, component labels, drawings, photos and a description of the required result. We will clarify which details must be confirmed before a quotation or technical recommendation.