Carton forming machine fold cracking can originate in the supplied blank, the forming sequence or both. Increasing forming pressure may make a carton close while worsening a damaged crease. The first decision is whether the material already has a weak fold or the machine is forcing it along the wrong path.
This guide focuses on paperboard hamburger and food cartons. Use the approved blank drawing, board grade and crease specification. Packaging appearance, structural strength and any barrier requirements need their own acceptance criteria; a visible white line alone does not describe every failure mode.
Diagnostic decision table
| Observed pattern | Comparison sample | Likely investigation |
|---|---|---|
| Cracking during controlled off-machine fold | Unprocessed blank from the same lot | Board and crease preparation |
| Cracking only on the machine | Same blank and fold direction | Sequence, alignment and contact |
| One panel repeatedly affected | Mark blank orientation | Local crease or tooling contact |
| Change appears after a board lot change | Accepted previous lot | Material and converting variation |
Classify the damage before adjusting the machine
Photograph the crease before and after forming under consistent lighting. Identify coating whitening, surface cracking, delamination or a tear through the board. Mark the affected panel, print side and feed direction on the blank drawing. Keep representative samples rather than only the most severe failure.
Ask the quality team which defects are unacceptable for the intended carton. A surface appearance issue and a structural split require different verification. Do not infer barrier performance from a photograph; use the agreed product test where barrier integrity matters.
Compare off-machine and machine folding
Fold controlled samples by the agreed test method in the intended direction and sequence. This is a diagnostic comparison, not an uncalibrated strength test. Record whether the crease bends at its intended location and whether the same damage appears without machine contact.
Iggesund identifies board moisture, thickness, grain direction and surface treatment as relevant to converting behavior. Check these against the approved specification and lot records. Avoid a universal rule about grain direction: the correct blank and crease design depends on the complete carton construction.
Inspect the supplied crease and blank
Compare crease position, consistency and visible damage with an accepted blank. Check whether the fold is centred on the crease or bends beside it. Review recent die-cutting changes and board substitutions with the blank supplier. A forming machine cannot reliably correct a crease outside the approved geometry.
Inspect storage and conditioning history, including exposure after unpacking. Keep board identity and elapsed exposure with the trial. Do not wet blanks to make them fold unless the material supplier has defined and approved that process; uncontrolled moisture changes can introduce additional variation.
Observe the forming sequence and contact
Using guarded observation or a safe video, determine which guide or forming tool first engages the affected panel. Compare the intended folding order with actual motion. Look for a corner trapped before its adjoining panel has moved and for guides that push beside the crease.
With energy isolated, inspect contact surfaces for burrs, buildup and sharp local damage. Review the related folding-rail procedure for the verified datum and changeover order. Correct alignment or a damaged surface before considering a pressure change that may merely hide the symptom.
Validate the correction at representative operation
Change one verified factor at a time and retain the original settings for comparison. Run approved blanks through startup and steady operation. Inspect each affected fold and check finished carton geometry, closing behavior and adhesive bonds after the required conditioning.
Record material lot, crease drawing, feed orientation, speed and the corrected machine setting. Send HANNAI both unformed and formed sample photos with the off-machine comparison. These records identify whether the next action is a blank-supplier correction, a tooling repair or a controlled setup change.
Related equipment and next checks
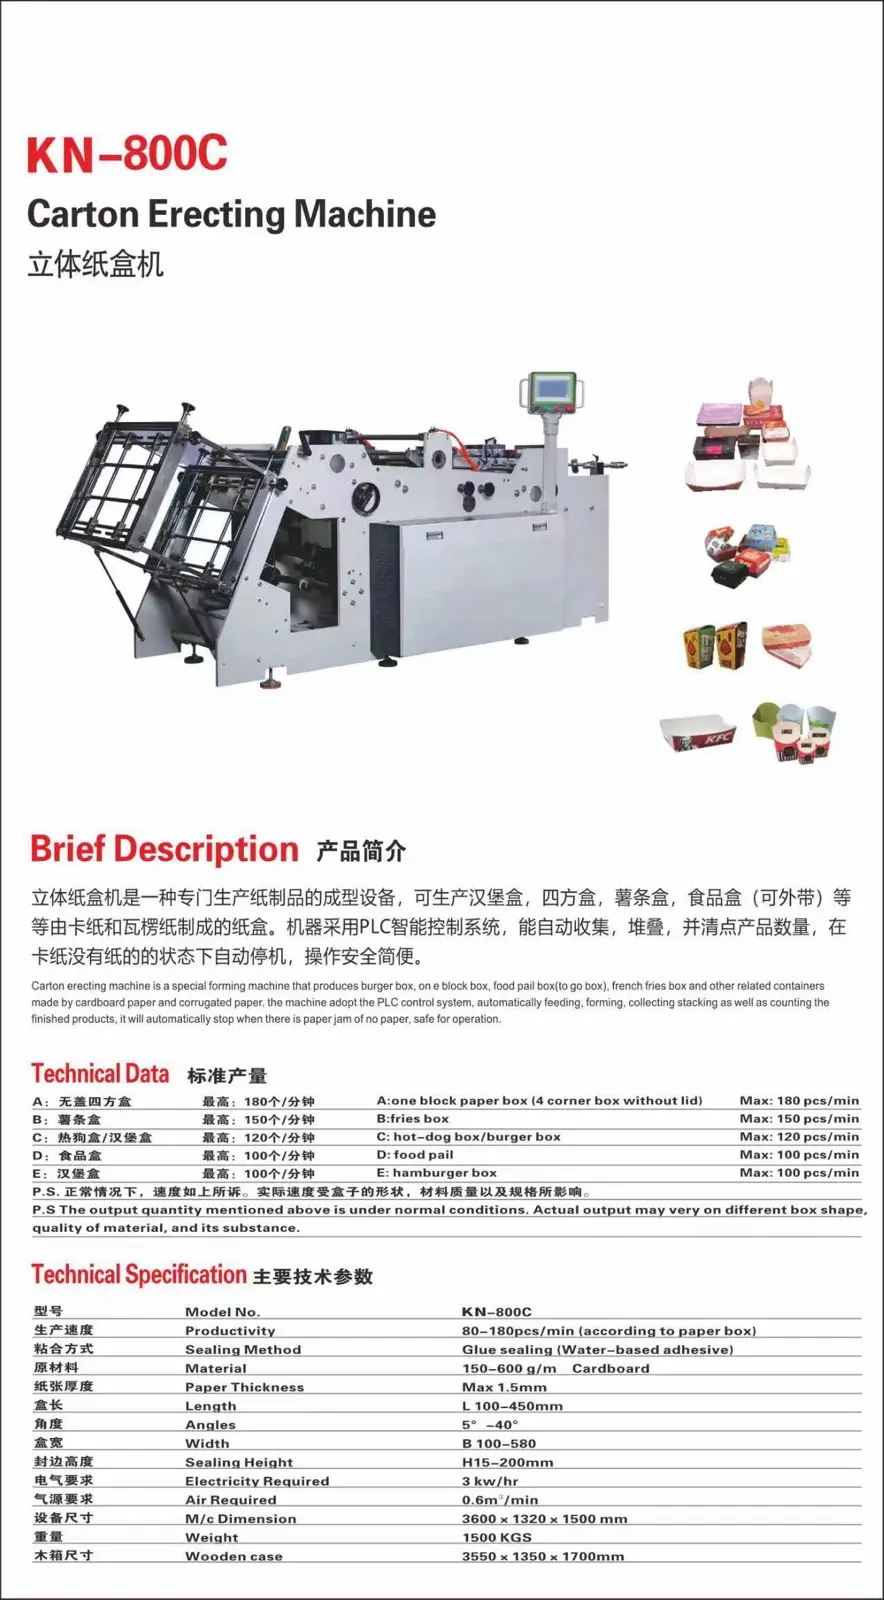
Review the carton forming machine and the related guide to folding rail changeover setup. The Engineering Notes archive connects these checks with wider machine planning.
Technical reference
- Iggesund die-cutting and creasing guidance — general reference; confirm applicability to the installed equipment.
Frequently asked questions
Should forming pressure be increased first?
No. Compare blank quality, fold location and sequence first.
Why test the same blank off the machine?
It helps separate material/crease behavior from machine contact.
Can a board substitution affect folding?
Yes. Check its approved construction and converting properties.
What evidence helps the supplier most?
Unformed and formed samples, lot identity, crease drawing and fold sequence.
Review the evidence with HANNAI
Send your machine model, component identification and the observations described in this guide. Include the drawing or material reference and any before-and-after measurements so the required next check can be identified.