A paper cup machine maintenance backlog is more than a list of overdue work. It represents unresolved asset conditions with different consequences for safety, cup conformity, availability and cost. Effective prioritization makes the decision criteria visible and keeps temporary controls from silently becoming permanent.
This guide supports maintenance planning. It does not set universal risk scores, service intervals or repair methods. Follow the machine manual, site safety rules and authorized engineering decisions.
Diagnostic decision table
| Backlog factor | Evidence to review | Weak shortcut |
|---|---|---|
| Safety consequence | Hazard and control status | Age of request only |
| Quality consequence | Defect and detection relationship | No current complaint |
| Failure likelihood | Condition and history | Operator opinion alone |
| Work readiness | Parts, skills and access | Schedule without resources |
Create one controlled backlog
Bring open inspections, operator reports, breakdown follow-ups, temporary repairs, calibration findings and planned work into one controlled register. Assign a unique item, machine location, observed condition, originator, date, owner and status. Link photographs, alarm history and measurements without replacing the original report.
Remove duplicate entries only after their relationship is confirmed. A closed duplicate must point to the surviving item. Do not hide waiting work in personal notes or shift messages because planners then cannot see total exposure.
Assess consequence before urgency
Evaluate credible effects on people, guarding, heating, electrical control, compressed air, cup sealing, dimensions, detection and packing. Consider what happens if the condition worsens during startup, steady production or changeover. Separate current evidence from a hypothetical worst case.
High-consequence conditions require escalation even when failure frequency is low. Production demand cannot lower the technical consequence. Define any immediate stop, isolation or containment requirement through the approved safety and quality processes.
Estimate likelihood from condition evidence
Use inspection results, wear trends, repeat alarms, leakage, temperature behavior, vibration, cycle counts and repair history as applicable. Record uncertainty and the date of evidence. A component that looked acceptable months ago may need reassessment before priority is confirmed.
Avoid converting sparse history into a precise failure probability. Use consistent categories that planners understand. When evidence is weak, schedule an inspection or diagnostic task rather than pretending the repair decision is certain.
Check readiness and dependencies
Identify parts, drawings, tools, access, isolation, qualified personnel, production window and verification method. Some high-priority work cannot start safely until these dependencies are ready, but readiness should be accelerated rather than used to reduce risk ranking.
Group tasks only when shared shutdown or access reduces exposure without expanding scope beyond control. Protect critical work from being displaced by easy low-value tasks that improve completion counts but leave important risk open.
Review ageing and temporary controls
Set review frequency by risk and condition. Confirm that temporary controls remain installed, effective and understood. Escalate items whose evidence worsens, due date passes or assumptions change. Record deferral approval and the next decision point.
ISO 55001:2024 frames asset decisions around value, performance, risk and expenditure. Apply the purchased standard through the site system. Send HANNAI the backlog item, machine identity and condition evidence when supplier input is needed.
Related equipment and next checks
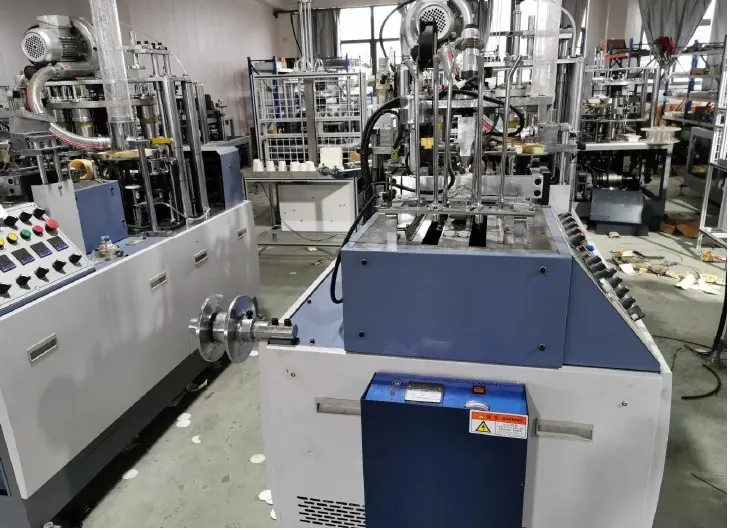
Review the HN-M100 automatic paper cup machine and the related guide to paper cup machine maintenance checklist. The Engineering Notes archive connects these checks with wider machine planning.
Technical reference
- ISO 55001:2024 asset management overview — general reference; confirm applicability to the installed equipment.
Frequently asked questions
Should the oldest task always come first?
No. Prioritize consequence, condition and readiness while monitoring age.
Can production demand lower a safety priority?
No. Apply authorized safety and risk controls.
How are deferred tasks controlled?
Record approval, temporary controls and the next review point.
What if likelihood evidence is weak?
Plan inspection or diagnosis and state the uncertainty.
Review the evidence with HANNAI
Send your machine model, component identification and the observations described in this guide. Include the drawing or material reference and any before-and-after measurements so the required next check can be identified.