A paper cup reject system challenge test checks whether a defined detectable defect is recognized, tracked and physically removed from accepted output. A reject signal on the HMI proves only one part of that chain. The test must also account for every challenge cup and the nearby acceptable cups.
Use an approved quality-system test plan for the installed inspection equipment. This is not a safety-interlock test. Never introduce foreign objects, deliberately jam tooling or bypass guards to create a defect. Where the machine lacks the relevant detector, do not claim that it can reject that defect automatically.
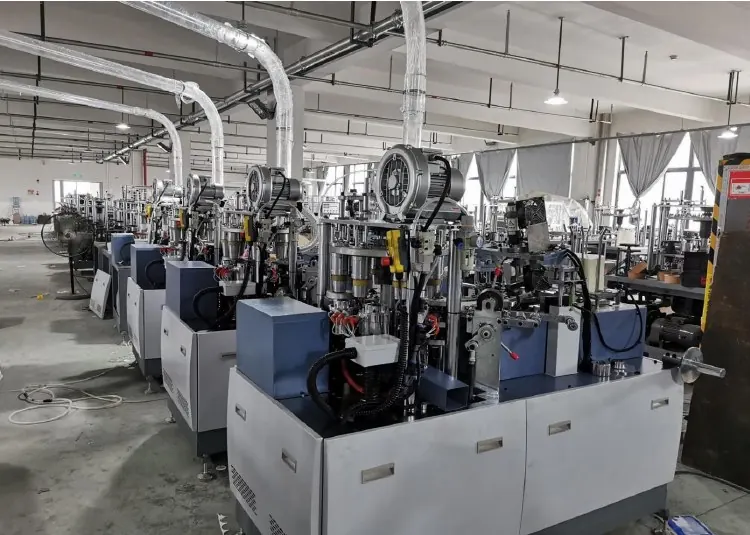
Diagnostic decision table
| Stage | Evidence to collect | Failure to distinguish |
|---|---|---|
| Detection | Correct event for identified challenge | Missed detection |
| Tracking | Correct cup identity through transfer | Timing or identity mismatch |
| Removal | Challenge reaches the reject destination | Actuation or chute failure |
| Containment | All challenge pieces recovered | Test material mixed with accepted stock |
Define the detectable defect and test location
Confirm what the installed system is designed to inspect and what it cannot see. Identify the relevant recipe, sensor or vision program and the approved quality acceptance rule. A detector intended for cup presence cannot be assumed to detect a weak seal or a dimensional deviation.
Agree an OEM-approved challenge sample or simulation method that represents the intended detection condition without risking machinery damage or contamination. Define where and how it can be introduced safely. If only a software diagnostic simulation is possible, state that it checks logic rather than the complete physical detection-to-rejection chain.
Identify and contain every challenge sample
Assign durable sample identities using a marking method approved for the test and product environment. Count the samples before the trial and define their final collection and quarantine location. Include any machine buffer or collection stack that could hold a challenge after the apparent end of the test.
Prevent challenge material from entering saleable stock. Use the approved line-clearance and product-hold procedure, with a responsible person controlling the test. Avoid informal demonstrations during unrestricted production. If a challenge sample cannot be accounted for, follow the containment procedure rather than assuming that it must have been rejected somewhere.
Observe detection and physical outcome separately
Record the challenge identity, introduction sequence, detector result and final destination. Include acceptable control cups before and after the challenge so the test can reveal a tracking offset that rejects a neighbor instead of the intended cup. Preserve the normal guarding and permitted observation arrangement.
Where the system provides event timestamps or counters, capture them without clearing the prior evidence prematurely. Compare a counter increment with the actual recovered sample. A signal can be generated even when the reject mechanism fails to move the cup, and a cup can leave the line through a jam rather than a correct reject action.
Cover the operating conditions in the claim
Agree the relevant speed, spacing, cup specification and permitted stop-restart conditions with the supplier. A test at slow demonstration speed supports only that condition unless the plan includes normal operating behavior. Use an appropriate number of repetitions and sequence patterns; a single successful removal is a functional observation, not a quantified detection-performance guarantee.
Record false rejects of acceptable controls separately from missed challenges. If a failure occurs, retain the identity sequence and event log for diagnosis. Do not force PLC bits or extend rejection duration indiscriminately to obtain a passing demonstration, because that can hide the original tracking problem and increase good-product losses.
Close the trial with reconciliation and retesting
Reconcile every introduced challenge, clear the defined product path and retain the signed test record. State which stages passed and which were simulated or not tested. Restore approved production configuration through the normal release process and verify that the correct inspection recipe remains selected.
Send HANNAI the equipment configuration, challenge definition, event sequence and recovered-sample results if the outcome is inconsistent. After an authorized correction, repeat the failed condition and the relevant controls. Keep the original failure record; it explains why the corrective action was needed and supports a more useful verification than a final photograph of a full reject bin.
Related equipment and next checks
Review the HN-M100 production configuration and the related guide to reject chute and removal diagnosis. The Engineering Notes archive connects these checks with wider machine planning.
Frequently asked questions
Does an HMI reject count prove physical removal?
No. Check the destination of the identified challenge cup.
Can a normal cup-presence sensor detect every defect?
No. Detection scope depends on the installed inspection system.
May a foreign object be inserted to test rejection?
Use only approved safe challenges; do not risk contamination or machine damage.
What if a challenge cup is missing after the test?
Apply the defined containment and line-clearance procedure before product release.
Review the evidence with HANNAI
Send your machine model, component identification and the observations described in this guide. Include the drawing or material reference and any before-and-after measurements so the required next check can be identified.